WQT — Weld Quality Technologies
Let's talk
Services Management Compliance Sectors Our work Approach Standards Contact Email WQT
WQTIndependent welding & quality expertise

Quality built into every weld.

WQT provides quality management, welding coordination, project QA/QC and operational support for industrial piping and steel fabrication — from the ISO management system and EN 1090 / ASME IX readiness to the final handover dossier.

ISO 9001Quality systems
EN ISO 3834Welding quality
EN 1090& ASME IX readiness
QA / QCProject assurance
Welding inspector checking a ground butt weld on a stainless steel process pipe with a weld gauge Piping · Fabrication · Assurance
Weld inspectionVerified at the joint, recorded in the dossier.
01What we do

One partner. Complete quality oversight.

Practical quality management that works in the office, in the workshop and on site — built on the standards your clients and notified bodies audit against.

01

Quality management systems

ISO 9001 gap analysis, process mapping, documented procedures and records, internal audits to ISO 19011, corrective actions, management review and preparation for the certification audit.

ISO 9001→
02

Welding quality management

Alignment with EN ISO 3834-2/-3, welding coordination support to ISO 14731, WPS and WPQR to ISO 15609-1 / ISO 15614-1, welder and operator qualifications to ISO 9606-1, consumables control and welding records.

EN ISO 3834→
03

Project QA / QC

Project quality plans, inspection and test plans (ITPs), hold and witness points, inspection coordination, non-conformance (NCR) management and the interface with client, third-party and notified-body inspectors.

Project assurance→
04

Piping & fabrication quality

Weld maps and weld logs, material traceability against EN 10204 3.1 / 3.2 certificates, fit-up and visual inspection, dimensional control, PWHT and pressure-test witnessing, piping handover to EN 13480 or ASME B31.3.

Industrial piping→
05

NDT coordination & evaluation

NDT scope per code and specification (RT, UT / PAUT, MT, PT, VT), NDT requests and tracking, repair-rate monitoring, acceptance criteria to ISO 5817 or the applicable code, and coordination of NDT subcontractors.

Inspection & NDT→
06

Documentation & handover

Manufacturing data records (MDR), as-built weld dossiers, certificate packs, NDT reports, punch-list closure and turnover packages structured to pass client and end-user review the first time.

Final dossier→
02Management & operations

Beyond the weld. A company that runs on process.

Quality depends on how projects are run and how the company is organised. We bring structure to planning, workflows and daily operations — so good results are repeatable, not accidental.

07

Project management

Project set-up and execution plans, schedules and milestones, resource and cost tracking, risk and change registers, progress reporting and coordination of subcontractors, suppliers and client interfaces.

Planning & control→
08

Workflows & processes

Process mapping from enquiry to invoice, clear responsibilities (RACI), standard operating procedures and work instructions, document control, digital forms and the removal of bottlenecks and duplicate work.

Process design→
09

Operations management

Workshop and site organisation, production planning and capacity, KPIs such as on-time delivery, repair rate and cost of quality, lean and 5S practices, and management reporting that supports decisions.

KPIs & efficiency→
10

Organisation & competence

Organisation charts, roles and job descriptions, competence and qualification matrices, training plans and the appointment of responsible persons — welding coordinators, QC inspectors, coating inspectors.

People & roles→
11

Supply chain & subcontractors

Supplier and subcontractor qualification and evaluation, purchasing specifications that carry the technical requirements, incoming inspection and the control of outsourced processes such as NDT, PWHT and painting.

Supplier control→
12

Integrated ISO management systems

One integrated system for quality, environment and occupational health & safety — ISO 9001, ISO 14001 and ISO 45001 — with shared processes, risk-based thinking, internal audits and a single management review.

ISO 9001 · 14001 · 45001→
03Compliance & certification readiness

The standard your client asks for. Ready for audit.

A tender, a new client or CE marking requires a specific code? We prepare your company for it — procedures, qualifications, records and people — and stand beside you at the audit.

EN 1090-2 Execution of steel and aluminium structures

Preparation for factory production control (FPC) certification to EN 1090-1 and CE marking of structural steel components.

  • Execution class (EXC1–EXC4) determination
  • FPC manual, procedures and records
  • Welding coordinator appointment to ISO 14731
  • WPQR to ISO 15614-1 and welder qualifications
  • Declaration of Performance (DoP) and CE marking
  • Preparation for the notified-body audit
Step-by-step roadmap
EN 1090-1EXC1–4CE · DoP
ASME IX Welding, brazing and fusing qualifications

Qualification of procedures and personnel to ASME BPVC Section IX for ASME B31.3 piping, Section VIII vessels and US-specification projects.

  • WPS and PQR development and review
  • Welder and operator qualifications (WPQ / WOPQ)
  • P-numbers, F-numbers and essential variables
  • Qualification ranges matched to the project scope
  • Bridging existing ISO qualifications where accepted
  • Readiness for client and authorised-inspector review
Step-by-step roadmap
WPS · PQRWPQASME B31.3
EN ISO 12944 Corrosion protection by protective paint systems

Specification, control and documentation of painting and coating work on steel structures, piping and equipment.

  • Corrosivity category (C1–CX, Im1–Im4) and durability
  • Paint system selection and coating specification
  • Surface preparation to ISO 8501-1 (e.g. Sa 2½)
  • Coating ITP, dew point and climate monitoring
  • DFT measurement to ISO 19840, adhesion testing
  • Painting records and coating handover dossier
Step-by-step roadmap
C1–CXDFTISO 8501-1
Step-by-step roadmaps

From first meeting to certificate.

From product scope to CE-marked steel components: the typical path to EN 1090-1 FPC certification.

  1. 01Scope & execution classDefine what you make and how demanding it is.
    • Products: components and kits, steel grades, thickness range
    • Processes: cutting, holing, welding, bolting, surface treatment
    • Execution class EXC1–EXC4 from consequence, service and production categories
    • Attestation route (system 2+) and selection of the notified body

    OutputScope and EXC statement

  2. 02Gap assessmentCompare what you have with what the standard requires.
    • Review of organisation, equipment, workshop and existing procedures
    • Welding quality level required: EN ISO 3834-3 for EXC2, -2 for EXC3/EXC4
    • Missing WPQRs, welder qualifications and coordinator competence
    • Calibration, traceability and inspection capability

    OutputGap report and prioritised action plan

  3. 03People & welding coordinationPut the right competent persons in place.
    • Responsible welding coordinator to ISO 14731, knowledge level matched to the EXC
    • Welder qualifications to ISO 9606-1, operators to ISO 14732
    • NDT personnel to ISO 9712, through staff or a subcontractor
    • Job descriptions, training and competence records

    OutputCompetence matrix and appointment letters

  4. 04Welding proceduresQualify the procedures your production really uses.
    • WPS to ISO 15609-1 for each process, material group and joint type
    • Qualification route by EXC: procedure test ISO 15614-1, pre-production test ISO 15613 or other permitted methods
    • Test coupons welded and witnessed by the examiner or notified body
    • Mechanical testing and NDT at an accredited laboratory

    OutputWPS / WPQR register

  5. 05FPC system & documentationWrite the factory production control system around how you work.
    • FPC manual: contract review, design input, purchasing and subcontracting
    • Material traceability with EN 10204 3.1 certificates and marking
    • Inspection and testing: 100% visual, supplementary NDT, ISO 5817 quality levels per EXC
    • Geometric tolerances, bolting, corrosion protection (link to EN ISO 12944)
    • Non-conformance, calibration, handling, storage and records

    OutputFPC manual, procedures and forms

  6. 06Implementation & internal auditProve the system works on a real job.
    • Run a live or pilot order through the full system
    • Weld logs, inspection reports, certificates and dimensional records
    • Internal audit against EN 1090-1 / -2 and EN ISO 3834
    • Management review and closure of findings

    OutputObjective evidence ready for the auditor

  7. 07Certification auditInitial inspection of the factory and FPC by the notified body.
    • Audit preparation and briefing of the key people
    • Support during the audit in the office and the workshop
    • Root cause and corrective actions for any findings

    OutputFPC certificate and welding certificate

  8. 08CE marking & surveillancePlace products on the market and keep the certificate.
    • Declaration of Performance (DoP) to the Construction Products Regulation
    • CE marking label and accompanying documents
    • Preparation for periodic surveillance audits and continual improvement

    OutputDoP, CE label and maintained certification

From code review to a qualified, controlled welding programme ready for client and inspector review.

  1. 01Code & scope reviewKnow exactly what has to be qualified.
    • Construction code: ASME B31.3, B31.1, Section VIII or Section I
    • Client specifications and any additional requirements
    • Base materials (P-numbers), processes, thickness and diameter ranges
    • Impact toughness, hardness and PWHT requirements

    OutputQualification matrix

  2. 02Preliminary WPSSet the variables before the test is welded.
    • Essential, supplementary essential and nonessential variables per QW-250
    • Filler metals by F-number and A-number
    • Preheat, interpass temperature and PWHT
    • Coverage planned so that few PQRs support many WPSs

    OutputpWPS set

  3. 03PQR test weldingWeld the test coupon under control.
    • Coupon preparation, material identification and traceability
    • Welding with actual parameters recorded pass by pass
    • Witnessing by the client or third party where required

    OutputTest coupon with recorded parameters

  4. 04Testing & PQRProve the procedure with the tests the code requires.
    • Tension tests (QW-150) and guided bend tests (QW-160)
    • Impact tests when toughness is required, hardness where specified
    • Testing at an accredited laboratory and review of results
    • PQR compiled and certified by the manufacturer

    OutputCertified PQR

  5. 05Production WPSIssue the procedures the welders will actually use.
    • WPS supported by one or more PQRs
    • Qualified thickness ranges per QW-451
    • Clear, shop-friendly format with all essential data

    OutputApproved WPS register

  6. 06Welder qualification (WPQ)Qualify every welder and operator for their range.
    • Test welds to the WPS
    • Bend tests, or volumetric NDE (RT / UT) as permitted by QW-191
    • Position and diameter ranges per QW-461 and QW-452
    • WPQ / WOPQ records and welder identification

    OutputWPQ records and welder ID list

  7. 07Continuity & controlKeep qualifications valid and the programme under control.
    • Six-month continuity log per process (QW-322)
    • Welder stamps, revocation and requalification
    • WPS / PQR register, revision control and consumable control

    OutputContinuity log and welding control procedure

  8. 08Client & inspector reviewBe ready when the documents are examined.
    • Document package for client QA and third-party review
    • Support for Authorized Inspector review on code-stamped work
    • Preparation for ASME certification programmes where pursued

    OutputReview-ready welding qualification package

From the corrosive environment to the coating dossier: how a durable, inspectable paint system is specified and delivered.

  1. 01Environment & durabilityDefine what the coating must withstand, and for how long.
    • Corrosivity category to part 2: C1–CX atmospheric, Im1–Im4 immersion
    • Durability range to part 1: low, medium, high or very high
    • Design for corrosion protection to part 3: edges, crevices, access

    OutputCorrosion protection basis of design

  2. 02Paint system specificationChoose a system that fits the category and durability.
    • Paint system to part 5: primer, intermediate and topcoat, nominal DFT
    • Duplex systems on hot-dip galvanised steel where needed
    • Laboratory performance test evidence to part 6 / part 9
    • Coating specification and product data sheets

    OutputCoating specification

  3. 03Surface preparationThe coating is only as good as the surface beneath it.
    • Rust grade and preparation grade to ISO 8501-1, e.g. Sa 2½
    • Edge and weld preparation grades P1–P3 to ISO 8501-3
    • Roughness profile to ISO 8503
    • Dust and soluble salt checks to ISO 8502

    OutputSurface preparation acceptance records

  4. 04Application controlControl the conditions while paint goes on.
    • Surface temperature at least 3 °C above dew point, humidity within limits
    • Stripe coats on edges and welds, overcoating intervals respected
    • Wet film thickness checks during application
    • Coating ITP with hold points, supervised by a qualified coating inspector

    OutputDaily painting and climate logs

  5. 05Inspection & testingVerify the finished system against the specification.
    • Dry film thickness measurement and acceptance to ISO 19840
    • Adhesion: pull-off to ISO 4624 or cross-cut to ISO 2409
    • Visual inspection for defects, holiday testing where specified

    OutputCoating inspection reports

  6. 06Documentation & reference areasLeave evidence that supports the guarantee.
    • Reference areas for long-term performance assessment
    • Batch numbers, certificates and inspection records compiled
    • Coating section of the handover dossier

    OutputCoating dossier

  7. 07Maintenance planningProtect the asset over its life.
    • Inspection intervals matched to category and durability
    • Assessment of coating degradation to ISO 4628
    • Maintenance and repainting specification

    OutputCoating maintenance plan

Typical sequence. The exact path depends on your products, your existing system and the certification body — we tailor it after the gap assessment.

04Who we work with

Demanding industries. Audited quality.

Fabricators, mechanical contractors and plant owners whose welds carry pressure, product and reputation.

  • Energy & powerPower plants, boilers, district heating, renewables balance-of-plant
  • Oil, gas & refiningProcess piping, tank farms, terminals and utilities
  • Chemical & pharmaClean stainless systems, orbital welding, high documentation demand
  • Food & beverageHygienic stainless piping, CIP systems, dairies and breweries
  • Shipbuilding & marineShip piping, repairs and class-surveyed work
  • Steel structures & EPCStructural steel fabricators, mechanical contractors and turnkey projects
05Where the work happens

From the arc to the dossier.

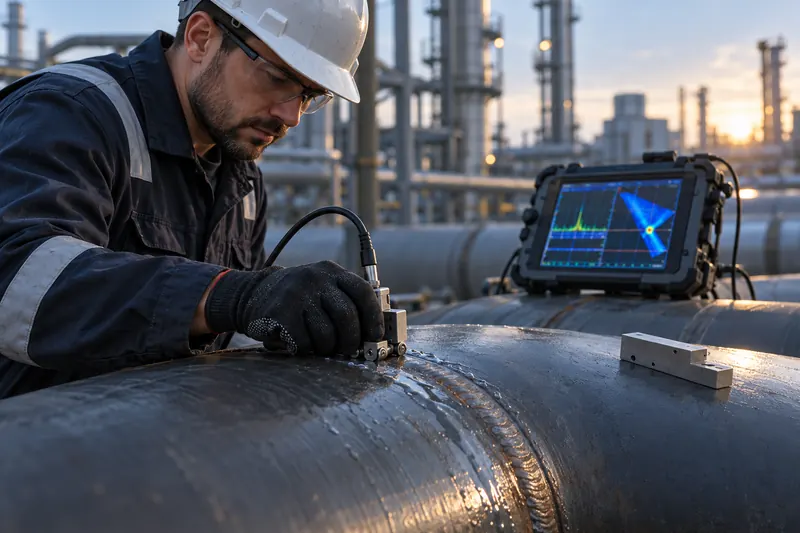
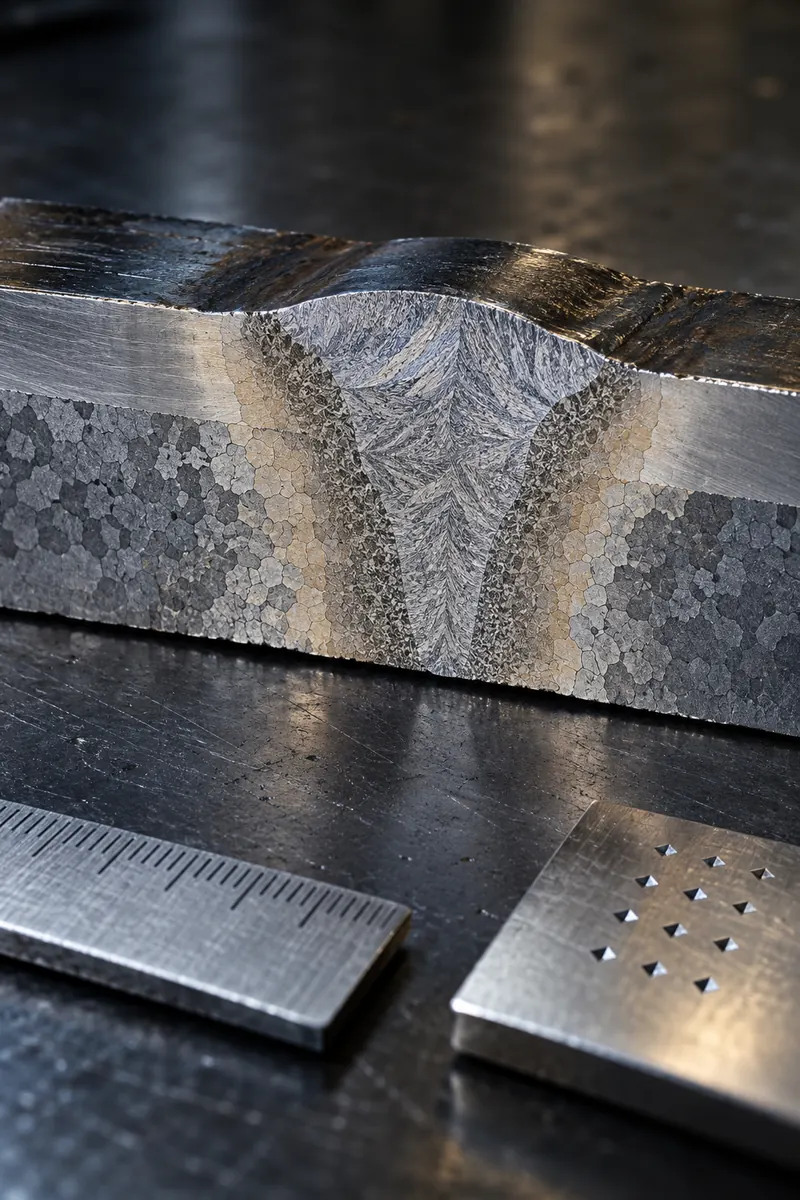
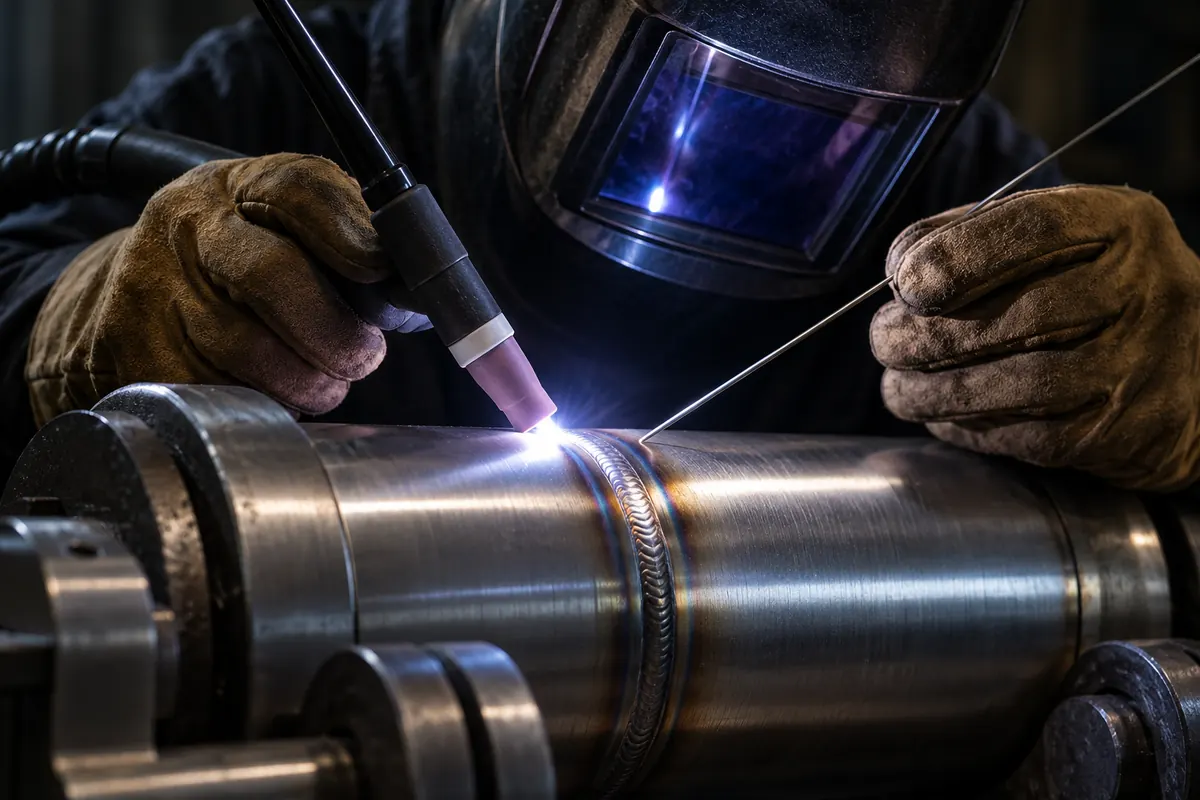
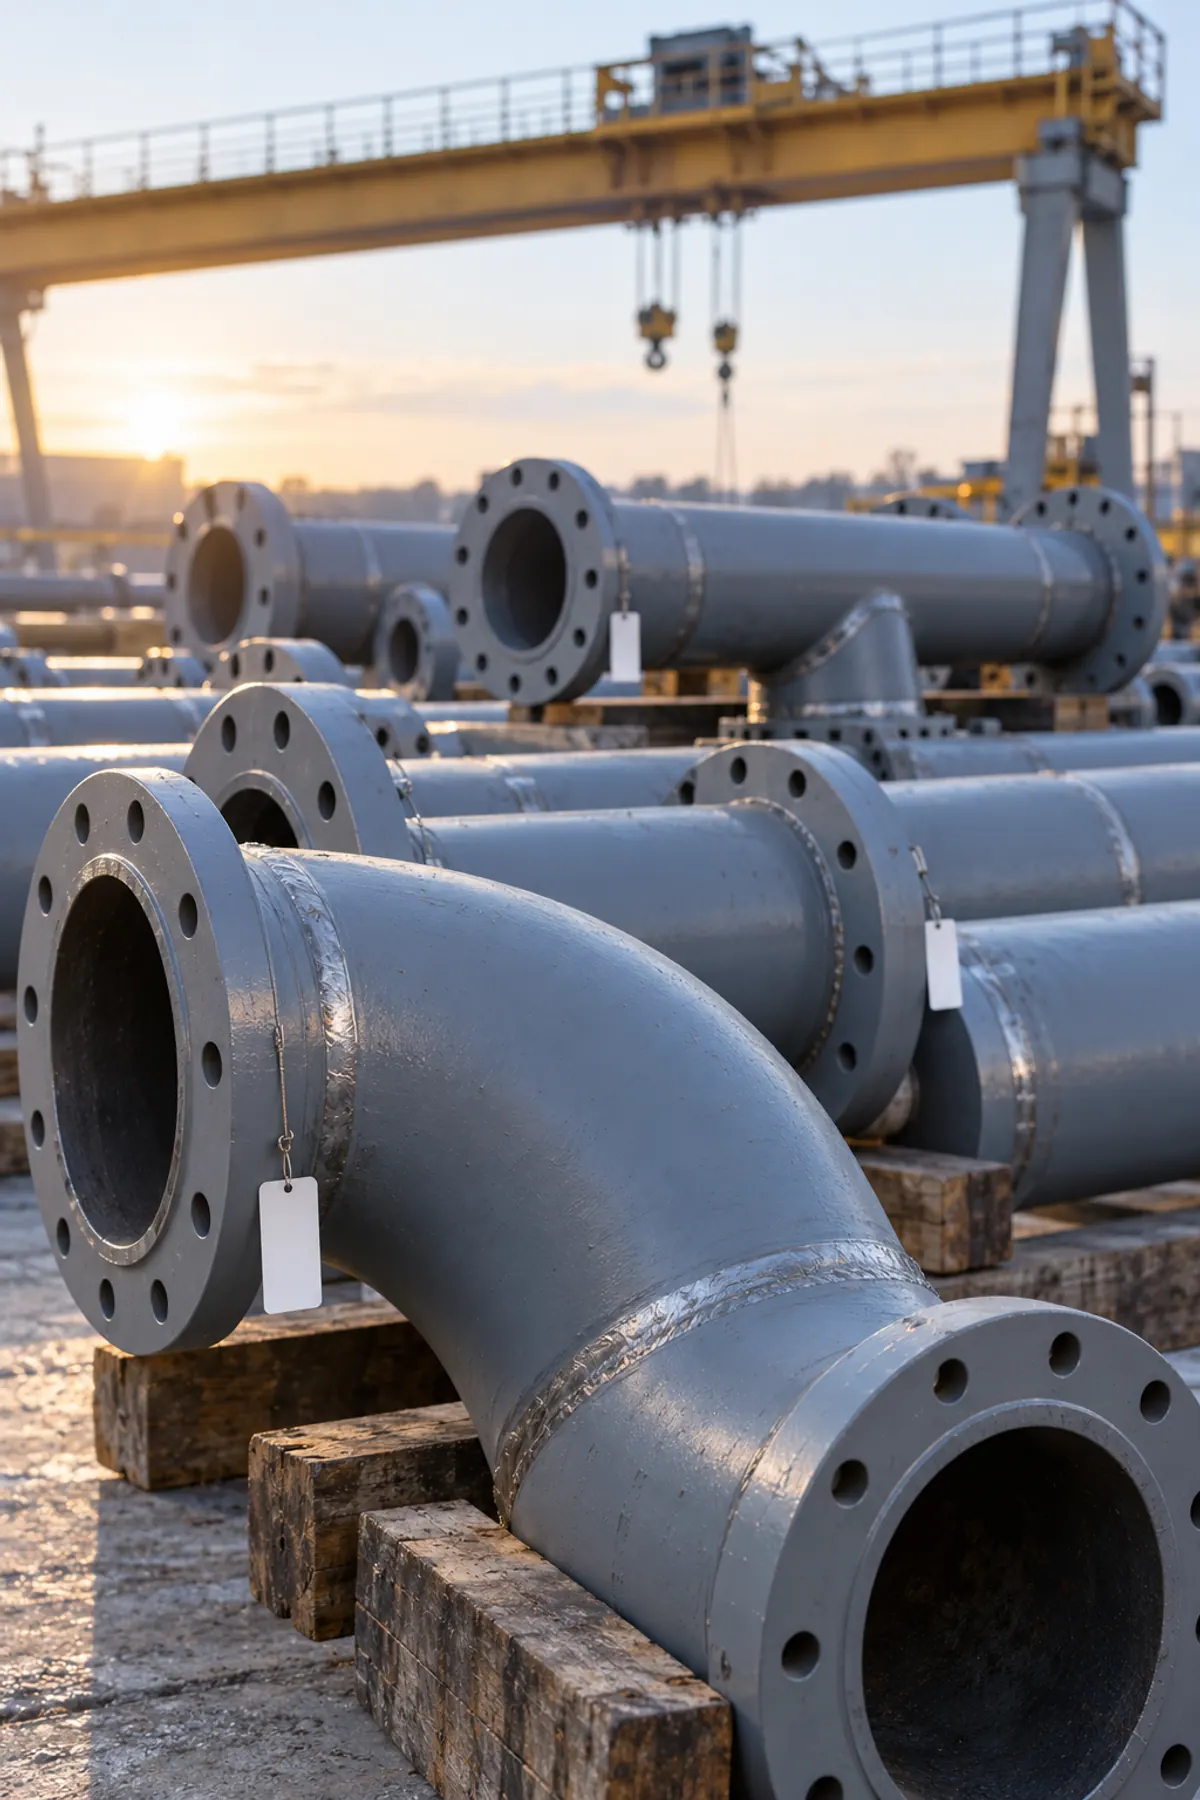
Quality is decided at the joint, proven by inspection and only counts once it is recorded. We cover all three.
WQTIndustrial quality

Built for demanding industrial environments.

Welding coordination, traceability, inspection and quality documentation that stand up to client review, third-party inspection and the pressure test — from the first drawing to the final dossier.

06What you receive

Deliverables your client can audit.

Every engagement produces documents that live on after we leave: the records a notified body, a class society or an end-user QA department will ask to see.

  • Project Quality PlanScope, organisation, responsibilities, applicable codes
  • Inspection & Test Plan (ITP)Hold, witness and review points agreed with all parties
  • WPS / WPQR registerProcedures matched to materials, thicknesses and positions
  • Welder qualification matrixValid ranges, expiry dates, prolongation records
  • Weld map & weld logJoint, welder, WPS, consumable heat, NDT result, repairs
  • Material traceabilityHeat numbers linked to certificates and to the installed joint
  • NCR registerDisposition, root cause, corrective action, closure evidence
  • NDT tracking & reportsRequests, coverage per code, repair rates, final reports
  • Final handover dossier (MDR)Indexed, complete and reviewed before it reaches the client
  • Audit-readiness packFPC or QMS manual, qualifications, internal audit and closed findings
07Our approach

Clarity at every critical stage.

We turn standards and contractual requirements into clear processes, accountable decisions and auditable evidence.

Two engineers reviewing a welding procedure on a tablet beside a welded stainless steel pipe assembly
Review at the joint: procedure, welder, record.
  1. 01

    Assess

    Define scope, contractual and code obligations, risks and the current quality maturity of your organisation or project.

  2. 02

    Structure

    Establish the quality plan, procedures, ITPs, welding documentation and the responsibilities that make them work.

  3. 03

    Verify

    Follow execution in the shop and on site, coordinate inspections and NDT, and resolve deviations while they are still cheap.

  4. 04

    Deliver

    Close actions, assemble the records and support the final handover, the certification audit or the client acceptance.

08Standards & frameworks

Built around recognised standards.

Standards provide the framework. Effective implementation delivers the value.

  • ISO 9001Quality management systems — Requirements
  • EN ISO 3834-2 / -3 / -4Quality requirements for fusion welding of metallic materials
  • ISO 14731Welding coordination — Tasks and responsibilities
  • ISO 15609-1 · ISO 15614-1Welding procedure specification and qualification (WPS / WPQR)
  • ISO 9606-1Qualification testing of welders — Fusion welding — Steels
  • ISO 5817Welded joints — Quality levels for imperfections
  • EN 13480 · ASME B31.3Metallic industrial piping · Process piping
  • PED 2014/68/EUPressure Equipment Directive — conformity assessment support, where applicable
  • ISO 19011Guidelines for auditing management systems
  • EN 1090-1 · EN 1090-2Execution of steel structures — FPC, execution classes and CE marking
  • ASME BPVC Section IXWelding, brazing and fusing qualifications (WPS / PQR / WPQ)
  • EN ISO 12944Corrosion protection of steel structures by protective paint systems
  • ISO 14001 · ISO 45001Environmental · Occupational health and safety management systems
  • ISO 21502Project, programme and portfolio management — Guidance on project management

WQT supports implementation of and alignment with the relevant requirements. Certification, accredited inspection and statutory approvals, where applicable, are issued by appropriately authorised third parties.

09Let's connect

Your next project deserves better quality control.

Setting up a management system, preparing for an ISO 9001, EN ISO 3834, EN 1090 or ASME IX audit, organising your operations or delivering a demanding project? Let's define the right quality approach together.

Start a conversation

Tell us what you're building.

Share your company, the scope and the quality requirements. We will come back with a tailored approach.

Email WQT
+30 693 660 9004 cragias34@gmail.com Christos Ragias · CEO Greece